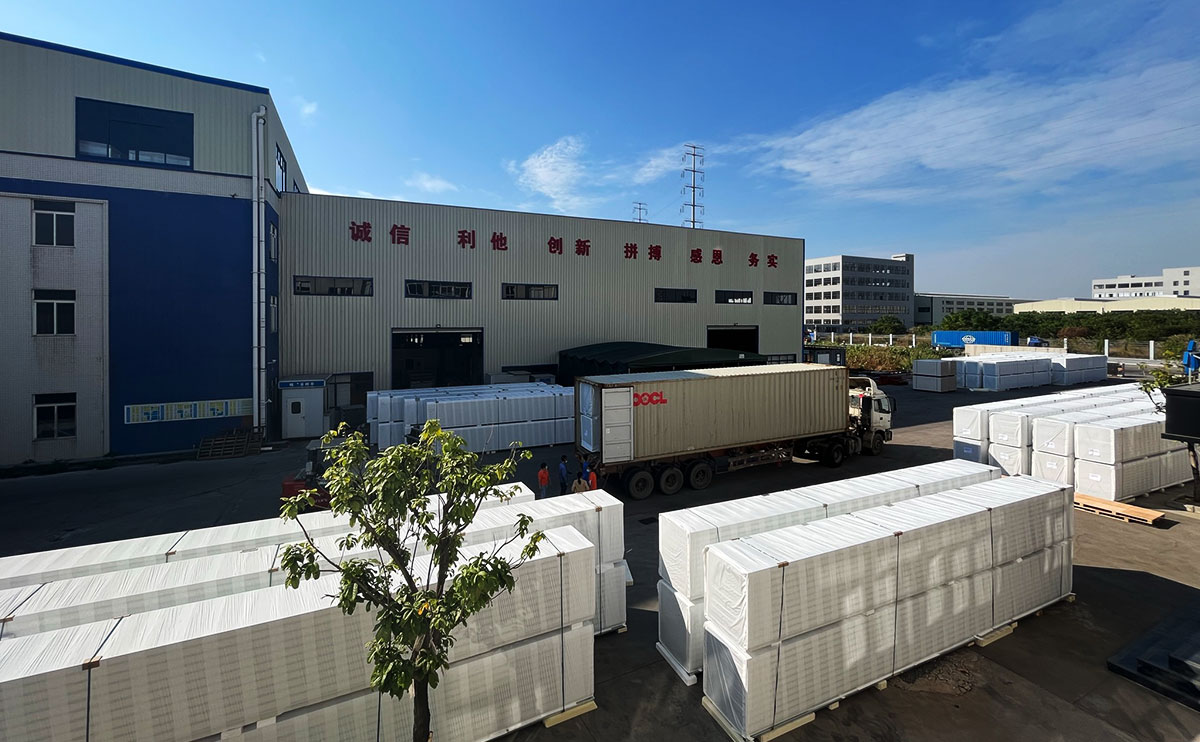
Professional custom sandwich panels manufacturer with more than 20 years of expertise — from medical-grade cleanroom panels to fire-rated wall & roof systems, delivered worldwide from our 20,000 m² Foshan factory.
Composite panels engineered for medical-grade, food-grade and laboratory-level environments — plus noise-reduction acoustic boards, cold room panels and fire-rated roof systems.
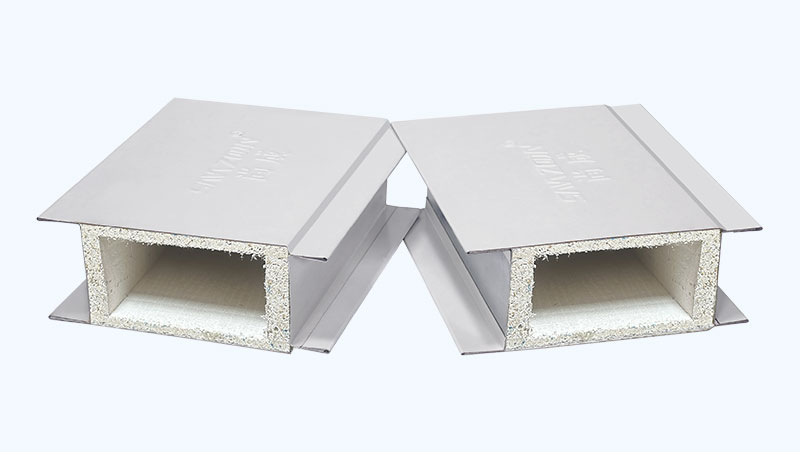
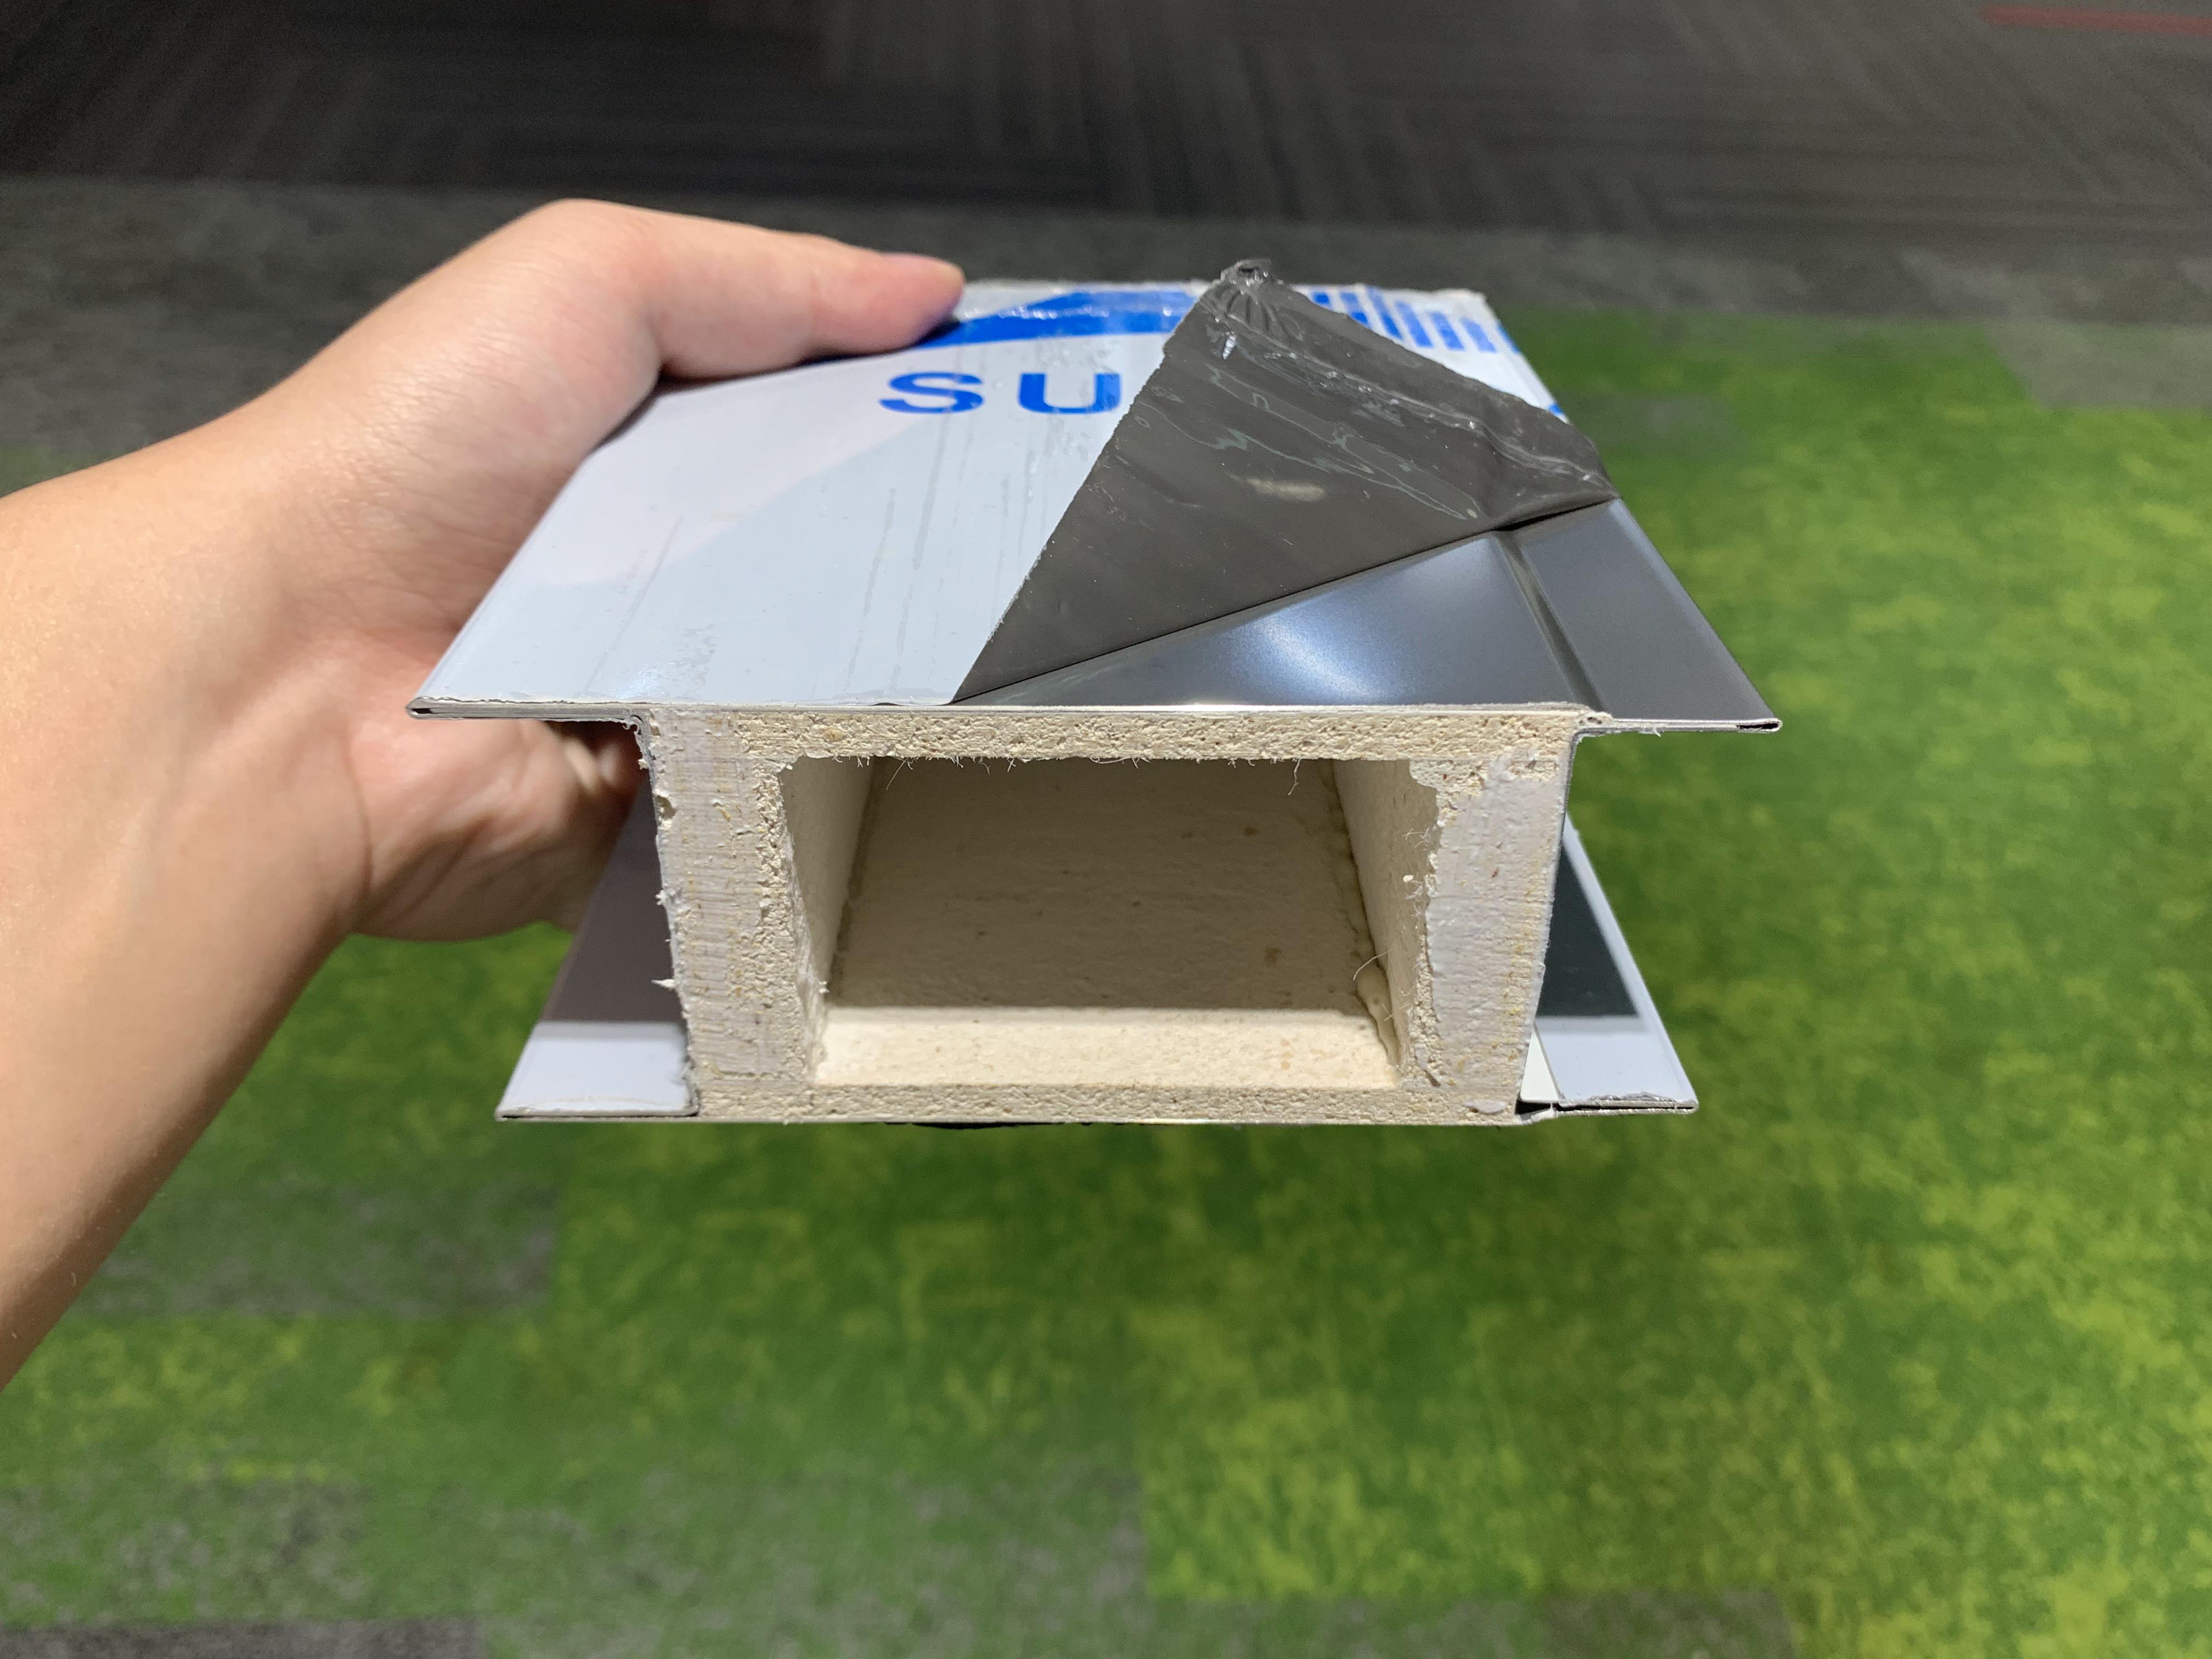
Class A1 non-combustible magnesium oxide core for cleanrooms and industrial walls.
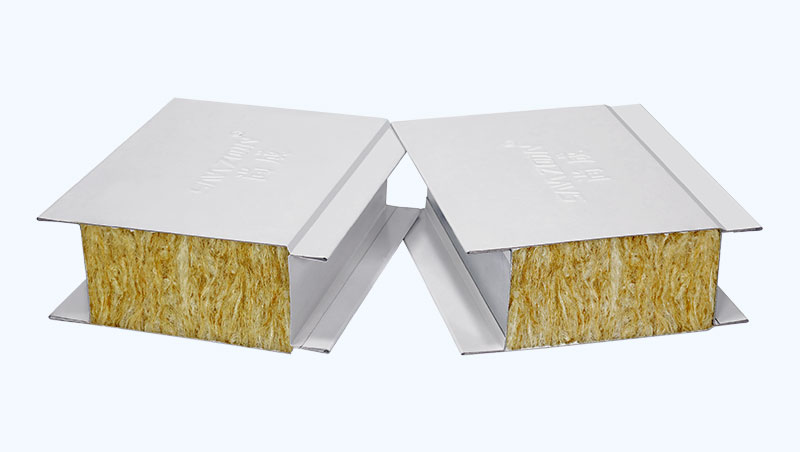
High-density rock wool core with superior fire, thermal and acoustic performance.
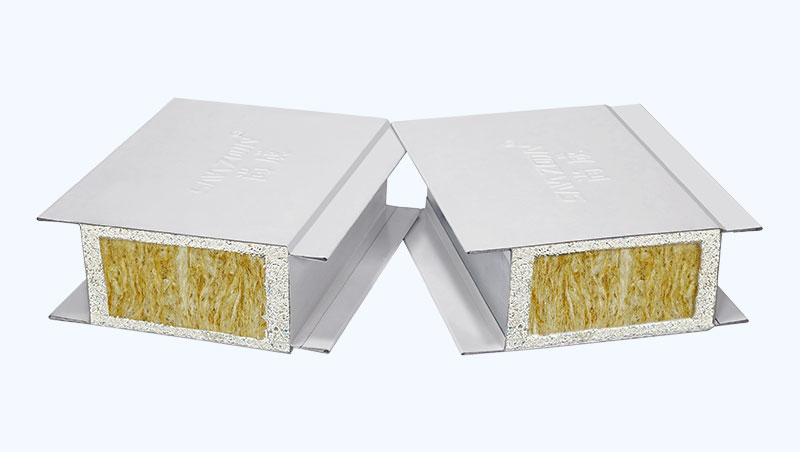
Hybrid MGO-framed rock wool panel combining structural strength with A1 fire rating.
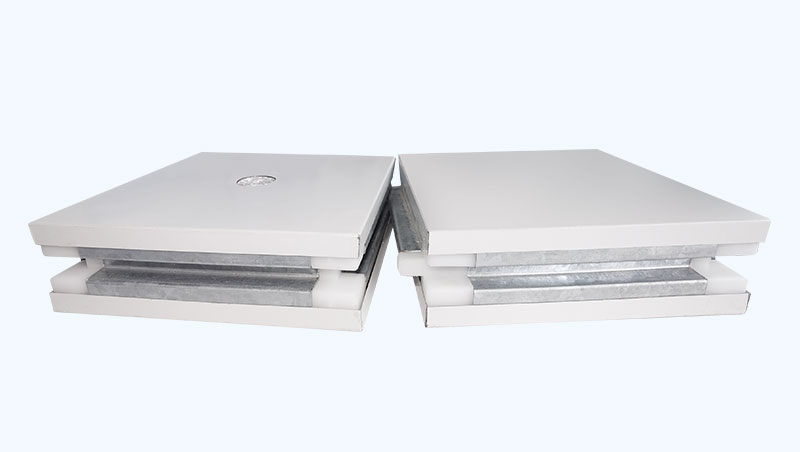
Aluminum-joinery handmade panels with superior airtightness for pharma & hospital cleanrooms.
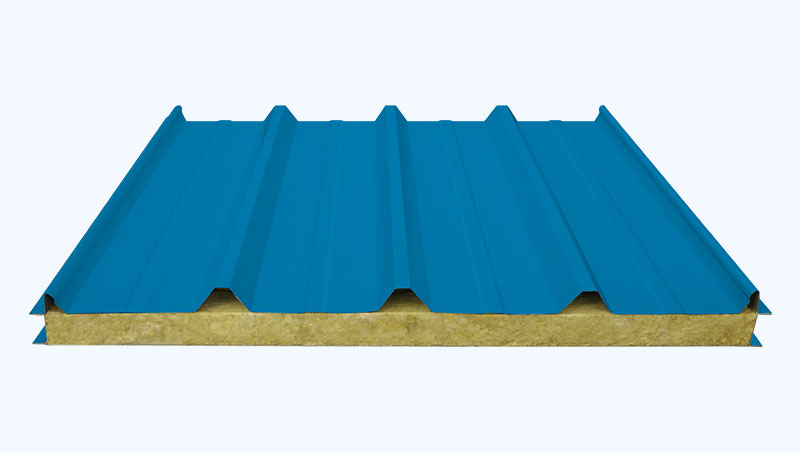
Corrugated rock wool roof panel for industrial plants — weatherproof and fire-safe.
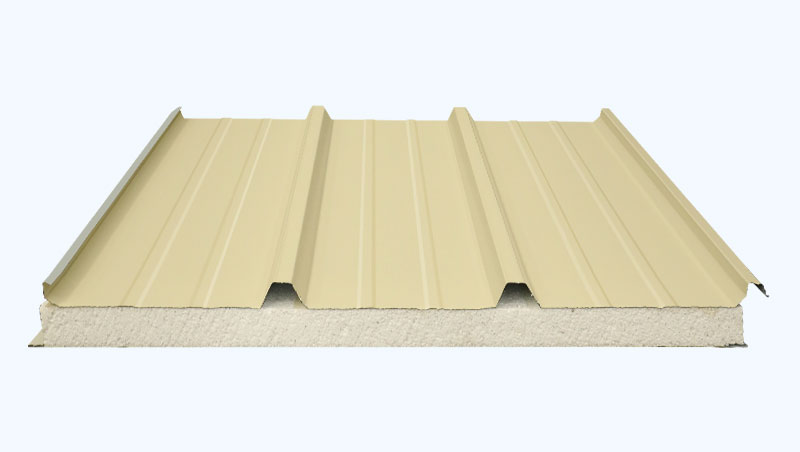
Wide-span insulated roof panel with fast lap installation for large buildings.
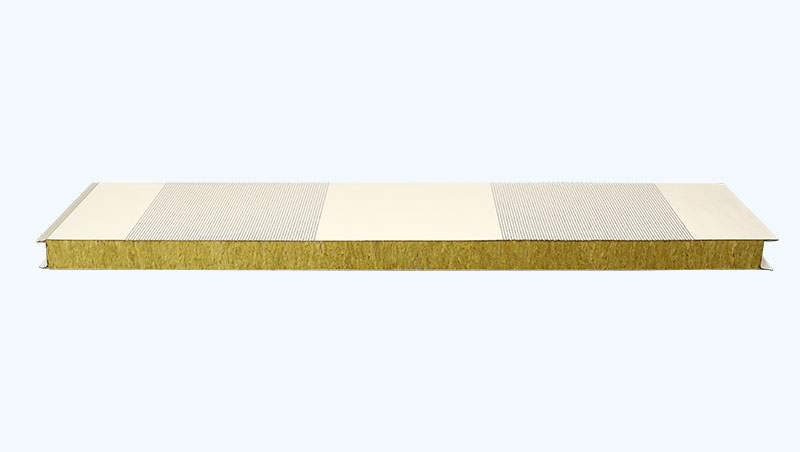
Perforated rock wool acoustic panels that cut reverberation in halls and factories.
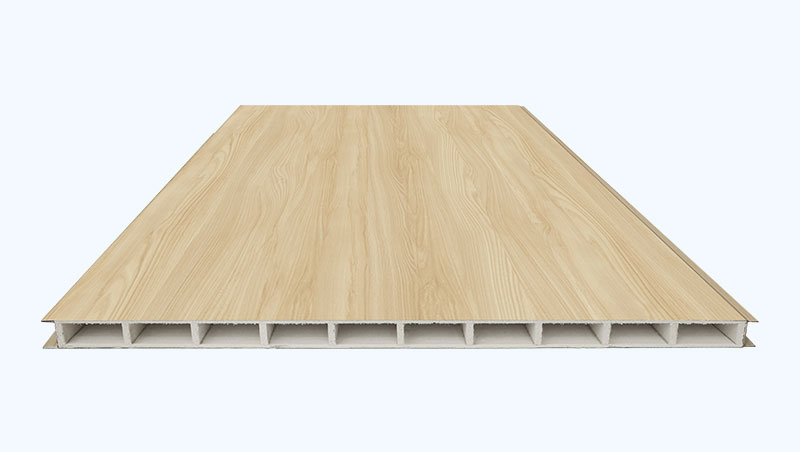
Wood-grain and custom-finish partitions for offices, hospitals and public spaces.
We work hard and fast while maintaining the quality and accuracy we are known for — a highly qualified team delivering better custom sandwich panels through continuous innovation.
Founded in 2015, our core team brings 18+ years of composite-panel expertise, with steady technical and management personnel providing a solid foundation.
Products exported to Australia, the United States, Europe, the Middle East, Russia, Southeast Asia and Africa — high market visibility and reputation.
ISO 9001 quality management, CE certification, 40+ national patents and 18 software copyrights — quality you can audit and trust.
Dedicated R&D, production management and marketing teams working in close cooperation to support every project from inquiry to after-sales.
Our panels are widely used in industrial plants, warehouses, hospitals, clean workshops, laboratories and modular buildings — delivering thermal insulation, fire protection and sound control.
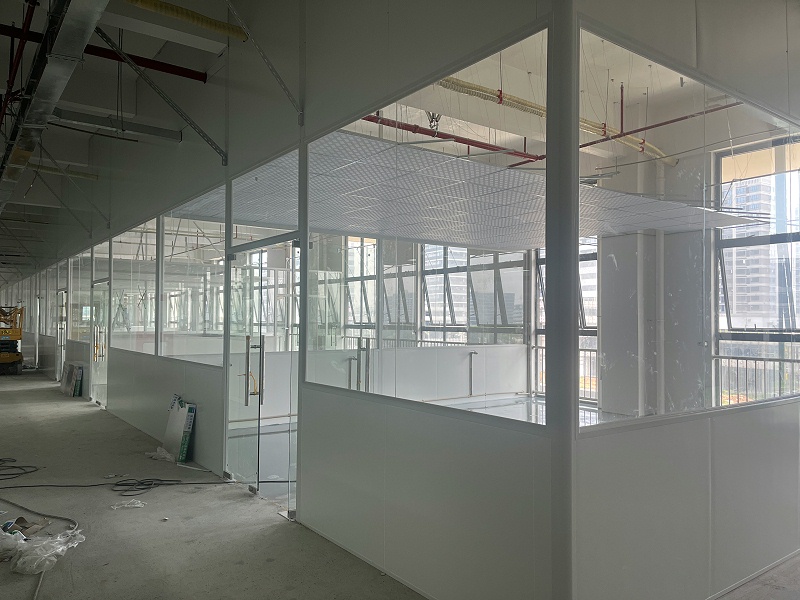
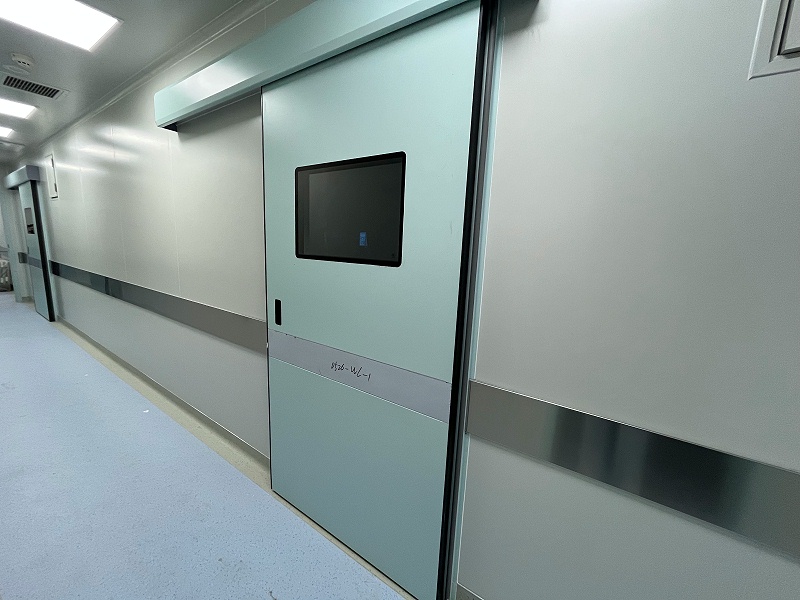
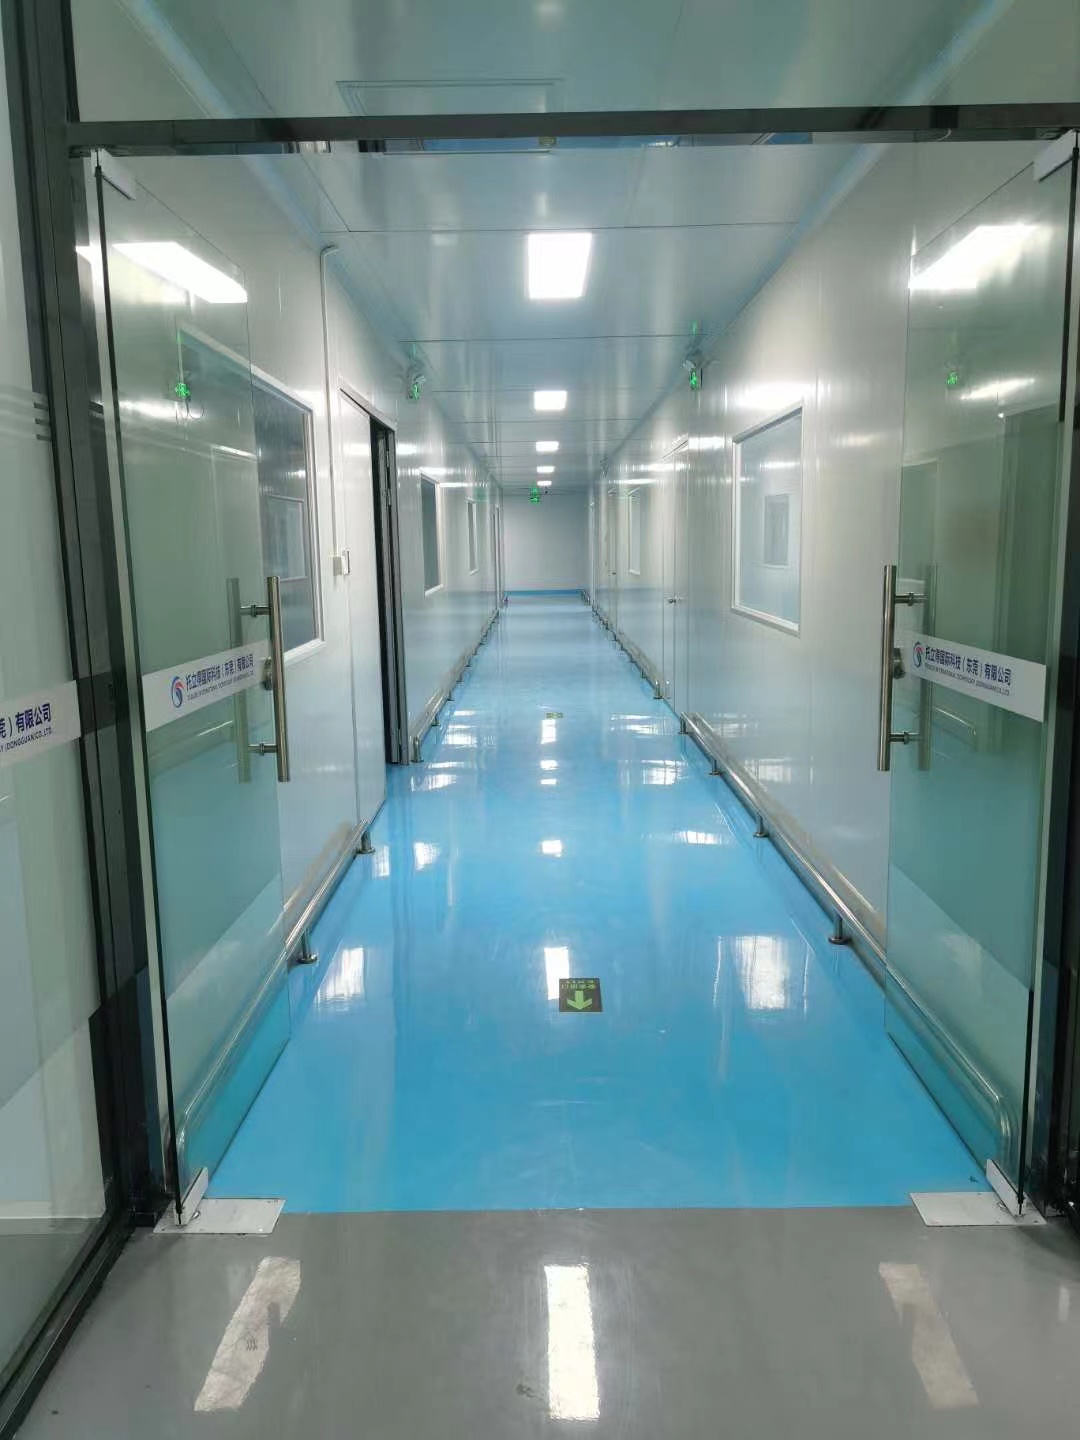
Hospitals, pharma plants, food & electronics cleanrooms with GMP-grade panels.
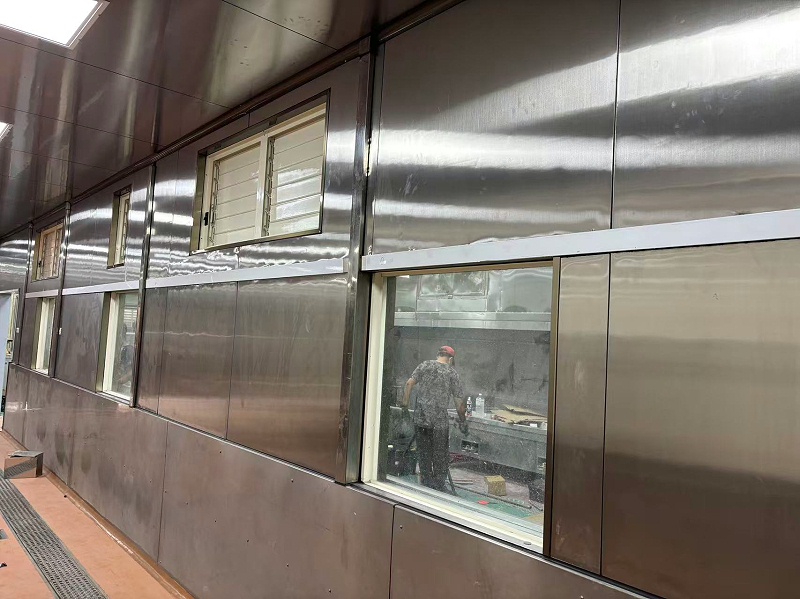
Cold storage and food processing facilities with insulated, moisture-proof panels.
Decorative partitions and acoustic walls for offices, airports and hospitals.
Container houses, prefabricated buildings and rapid-deploy enclosures.
From production to shipment — we promise every customer a one-stop service to ensure orders finish on time.
Clarify your specs, drawings, fire rating and budget requirements.
Site measurement and environment assessment when necessary.
Panel type, core material, thickness and connection solution design.
Transparent factory-direct quotation with volume discounts.
Automated lines with 10,000 m² daily capacity for fast lead times.
Full inspection of dimensions, bonding strength and surface finish.
Export-grade packaging; shipment from Foshan, Guangzhou or Shenzhen ports.
Remote or on-site installation guidance available when necessary.
Responsive after-sales support — quality you can rely on long-term.
We guarantee top-quality materials, reliability and customer-oriented working procedures — audited assurance for our customers.
From hospitals in Guangzhou to container-house exports for CIMC — see how SAMZOON panels perform in the field.
Zone-customized material strategy — wood-grain partitions in public areas, MgO clean panels in medical zones.
3,580 m² of A1 fireproof magnesium oxide panels enabling fast modular workshop zoning.
Class A non-combustible cleanroom walls and ceilings meeting UK food production standards.